Duiker Combustion Engineers
ACID GAS FIRED COMBUSTION EQUIPMENT
Flexibility in Design
The main reaction furnace is where the thermal stage of the modified Claus process takes place. In this thermal stage the majority of the sulphur recovered in the sulphur recovery unit is formed. Also impurities such as ammonia and aromatic hydrocarbons are destroyed here. The burner, naturally plays a crucial role in this through the degree of mixing achieved in the furnace as well as the temperature homogeneity that is reached. Furthermore, the flame stability generated by the burner plays a key role in the turndown that can reliably be met and the ability of the sulphur recovery unit to deal with upset conditions upstream.
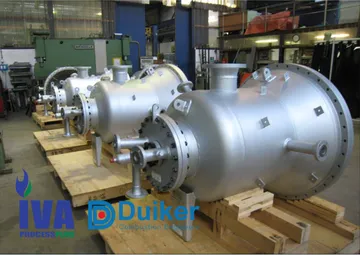
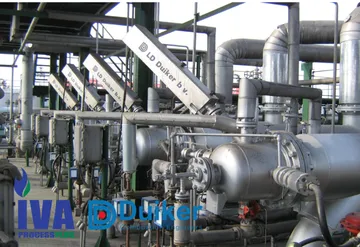

FUEL GAS FIRED COMBUSTION EQUIPMENT
Fuel Gas Firing in the Sulphur Recovery Unit
When we consider fuel gas fired combustion equipment in the sulphur recovery unit, we can distinguish between the substoichiometric in-line re-heaters and reducing gas generators and the superstoichiometric incinerator. Some design considerations remain the same for every piece of fuel gas fired process combustion equipment we design, namely: Safety, Performance and Reliability. However, some of the design criteria for these pieces of equipment are uniquely different.
STOICHIOMETRY-CONTROLLED OXIDATION
A Novel Concept
With refineries facing not only larger demand on their sulphur recovery capacity, but more and more, face capacity problems due to the quantity of sour water they generate, Duiker introduced a novel concept. This novel concept was sprouted from the idea that ammonia should be treated separately from a sulphur recovery unit as not only it increases the hydraulic load but its’ incomplete combustion can cause problems such as corrosive salt formation.